Hey folks, if you’ve ever sourced custom-machined copper parts—whether for electrical components, plumbing fixtures, or decorative hardware—you’ve probably heard the term “dimensional tolerance” thrown around a lot. As a copper turning supplier, I can’t stress enough how big a deal this actually is. I see so many shop owners, engineers, and hobbyists miss the mark on tolerances, either demanding way more precision than they need (and blowing their budget) or cutting corners so much that parts end up useless. Today, let’s break down what copper turning tolerances actually are, why they matter for copper specifically, and what you should expect when working with a copper turning vendor like me. Copper Turning
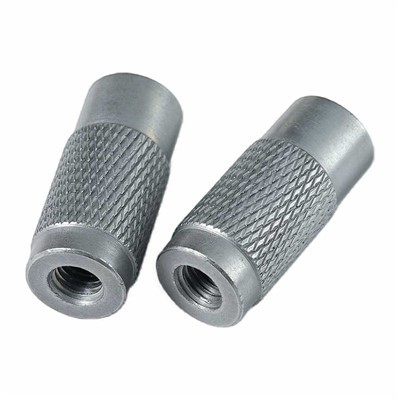
First off, let’s get the basics straight: what’s a tolerance, anyway? Super simply, it’s the maximum and minimum amount a dimension of a part is allowed to vary from the exact, perfect measurement you drew up. If you specify a hole needs to be 10mm in diameter, a tolerance of ±0.02mm means it can be anywhere from 9.98mm to 10.02mm and still work. Too tight a tolerance, and your parts are either impossible to machine (super slow, expensive, and likely to break tools) or end up rejected at inspection. Too loose, and parts won’t fit together, leak, or fail in use. It’s a balance, especially with copper, which is weirdly specific as a turning material.
Wait, why is copper different from, say, aluminum or steel? Let’s talk that out. Copper is soft—way softer than most alloy steels, and even softer than 6061 aluminum for many grades. That sounds like a good thing, right? More flexible, easier to machine? Not so fast. Soft metals have a quirk called “springback” or chatter when you’re turning them on a lathe. Chatter is that high-frequency vibration that makes the surface wavy, not smooth, and it’s way worse with copper because it’s soft enough to deflect under the cutting pressure, whereas stiffer steel holds its shape better. Also, copper has a tendency to form long, stringy chips when turned—those chips can get tangled in the tool, scratch the part, or even jam the lathe, which messes up dimensions mid-run. So even though it’s soft, machining copper to tight tolerances isn’t a walk in the park; you have to adjust your process specifically for it, which is why not every machine shop is good at consistent copper turning.
Now, what are the actual tolerances you can expect from copper turning, and how do they break down by part size and complexity? Let’s be real, there’s no one-size-fits-all number. Tolerances shift depending on how big the part is, how intricate its features are, and what grade of copper you’re using. The most common copper grades we work with are C110 (oxygen-free electronic copper, super pure), C260 (cartridge brass, which is a copper-zinc alloy, still pretty soft but a bit stiffer), and C360 (free-machining brass, with lead added to make it easier to cut—great for high-volume runs).
For small, simple turned parts—think a 5mm electrical pin, a tiny plumbing fitting nut, or a simple bushing that’s only got a few straight diameters or a single thread—we regularly hit tolerances of ±0.025mm (that’s 0.001 inches for my US-based folks). That’s pretty tight, right? But only if the part is simple. If you add more features: a counterbore, a cross-hole, a tapered section, or fine threads, that tolerance loosens up a bit to around ±0.05mm (0.002 inches) for most shops, including mine. Why? Because each extra feature requires a tool change, and every time you switch tools, there’s a tiny amount of alignment shift, even with the best CNC setups. For high-volume production runs—like 10,000+ identical small parts—we might even hold ±0.03mm, but that requires constant tool wear checks, in-process measurement every 50 parts, and even adjusting the lathe offset mid-run if needed.
Now, for medium-sized turned parts, say a 50mm diameter pump impeller housing or a custom valve body that’s around 100mm long, the tolerance range widens a bit. We typically see ±0.05mm to ±0.1mm (0.002 to 0.004 inches) here. The reason? Longer parts are more prone to deflection from the lathe’s chuck and tailstock pressure. If you’re turning a long rod, the end can vibrate more because it’s less supported, so holding tiny dimensions along the full length gets tricky. Big surprise—longer, bigger parts = slightly looser tolerances, all else equal.
What about large copper turned parts, like a 300mm diameter flange or a big custom electrical busbar end? For those, tolerances jump to ±0.1mm to ±0.2mm (0.004 to 0.008 inches) usually. At that size, even small temperature changes in the shop can affect the part. Copper has a high coefficient of thermal expansion—way higher than steel, actually. If you machine a part when the shop is 20°C (68°F), and then it sits in a customer’s facility at 30°C, it’ll expand slightly, so a tolerance that works at room temp might be off once the part is in use. That’s why for big copper parts, we always recommend specifying tolerances at a reference temperature (usually 20°C) and accounting for thermal expansion in the design. It’s a common mistake I see new customers make—they grab a tolerance spec from a steel part and apply it to copper, and wonder why their parts don’t fit later.
Wait, what about surface finish, since that ties into tolerances too? A lot of people mix these up, but surface finish (how smooth the part is, measured in Ra or RMS) is separate from dimensional tolerance, but they go hand in hand for copper. If a part has a rough surface from chatter, it might not seal right in a fitting even if the dimensions are within tolerance. For most copper turning, we get a surface finish of Ra 0.8 to 1.6µm (32 to 63 micro-inches) with standard tooling, and if you need smoother, like Ra 0.4µm (16 micro-inches), we can do that with diamond tooling or a light polishing pass after turning, though that adds a bit to the cost and lead time.
Now, let’s talk about what affects tolerances beyond part size and grade. First, machine tool type. CNC lathes are way more consistent than manual lathes for holding tight tolerances. A good CNC lathe with linear guides and a rigid frame can hold ±0.01mm on small, simple parts all day, while a manual lathe will struggle to get below ±0.05mm even for a skilled operator. That’s not to say manual shops are bad, but if you need consistent, repeatable tolerances for 1000+ parts, CNC is non-negotiable. Then there’s tooling. High-speed steel tools work for low-volume, rough cuts, but for tight tolerances and fine finishes, you need carbide tools, and for the smoothest surfaces, diamond tools. Cheap tooling wears out fast, which throws off dimensions mid-run—we always use premium tooling because we can’t afford to scrap parts due to worn inserts.
Also, material condition matters. Copper comes in extruded bars, rolled bars, and drawn bars. Extruded copper has a bit more internal stress from the extrusion process, so when you cut it on a lathe, it might spring back or warp as the stress is released, which wrecks dimensions. Drawn or rolled copper is more stable internally, so it holds tolerance better. That’s a small thing, but it’s why we specify drawn copper for precision turning jobs, even if it’s a tiny bit more expensive than extruded.
Now, when should you ask for tighter tolerances than the standard? Wait, let’s get real about this. Tighter tolerances = higher cost, longer lead times, higher scrap rates. You don’t need ±0.02mm for a decorative copper doorknob, or a bushing that’s going into a low-stress application. You only need tight tolerances when parts have to mate closely, seal, or fit into pre-existing assemblies. For example, if you’re making a copper connector that mates with a plastic housing, you need to hold tight OD tolerances to make sure it snaps in right. If you’re making a water valve seat, you need tight ID and surface finish tolerances to prevent leaks. If you’re over-specifying tolerances just because you “think it’s better,” you’re wasting money. I’ve had customers come to us with a spec of ±0.01mm for a part that only needs ±0.05mm, and we have to break it to them that they’re paying 3x more than they need to for that extra precision they’ll never use.
On the flip side, don’t loosen tolerances too much just to cut costs. If you specify ±0.2mm for a medical copper implant component (yes, we do those too!), that’s going to fail inspection, get rejected, and cost you way more in the long run. The sweet spot is always matching the tolerance to the application. If you’re not sure what tolerance you need, that’s fine—tell us your use case, and we’ll help you figure out the right balance so your parts work and don’t break the bank.
Let me give a couple real examples from our shop to make this concrete. Last quarter, we did a run of 2,000 C110 copper terminals for a electronics manufacturer. The terminals were 8mm long, with a 2mm OD pin and a 3mm ID receptacle. They needed to fit into a PCB socket with no wiggle, so we held ±0.02mm on both OD and ID. We used our CNC lathe with carbide tooling, ran at a moderate speed to reduce chatter, and checked every 100 parts with a micrometer and bore gauge. 99.8% of the parts passed inspection—only 4 were scrap, which is totally normal for a precision run of that size.
Another example: a custom copper pump impeller for a small water treatment system. It was 120mm in diameter, with 6 curved vanes, medium complexity, high volume (500 parts total). The customer didn’t need super tight tolerances, but they did need the vanes to spin true without vibration, and the OD to seal against a rubber gasket. We held ±0.08mm overall, which was perfect for their needs, kept the cost low, and the lead time was only 2 weeks. No issues with the parts once they got to the customer—they saved about 25% compared to if we’d held ±0.02mm for that job.
Wait, common mistakes people make with copper turning tolerances I should mention? Oh, so many. First, not accounting for thermal expansion. Like I said earlier, copper expands way more than steel. We had a customer a while back who machined a 200mm copper flange at 20°C, specified a gap between the flange and the housing of 0.1mm, and when the part was installed at 35°C, the gap closed completely—part seized. We had to remachine all 100 flanges, and that was a costly mistake because he didn’t tell us he’d be using it in a warmer environment. So always specify tolerance reference temperature, or adjust the gap accordingly.
Second, not allowing for thread tolerance. Threads have their own tolerance classes, right? For example, a UNF thread can have a tolerance of 6g or 6H. If you just specify “10mm thread” without a class, you might get threads that are too tight to screw on, or too loose and strip. Threads are a pain in copper because of that springback we talked about—soft copper can cause threads to deform if the tolerance is too tight. For most general use copper threads, we recommend 6H/6g classes, which are standard, and that translates to a pitch diameter tolerance of around ±0.05mm for 1mm pitch, which is perfect.
Third, not leaving enough stock for secondary operations. Sometimes people specify a final dimension, but forget that turning leaves a tiny amount of material (called “stock allowance”) for sanding, polishing, or plating. If you’re sending the copper part out for plating, you need to add 0.02 to 0.05mm of stock on all machined dimensions, because plating adds thickness (usually 0.01 to 0.03mm for common platings like nickel or tin). If you don’t add that stock, you’ll end up with parts that are too small after plating, or have to re-machine them, which is expensive.
Okay, so to wrap this up: dimensional tolerances in copper turning aren’t a one-size-fits-all number—they depend on part size, complexity, copper grade, application, and the capabilities of your machine shop. For simple small parts, expect ±0.02 to ±0.05mm; medium parts, ±0.05 to ±0.1mm; large parts, ±0.1 to ±0.2mm. Always match your tolerance to what the part actually needs—don’t over-spec to save money, don’t under-spec to the point of failure. Copper is a great material for all kinds of applications, but you have to work with its quirks (softness, thermal expansion, chip formation) to get consistent, accurate parts.
If you’re working on a project that needs custom copper turned parts—whether it’s electrical components, plumbing, automotive parts, medical devices, decorative hardware, whatever—hit us up. We specialize in precision copper turning, have years of experience working with all grades of copper, and will help you nail the right tolerances for your project so your parts work perfectly without breaking the bank. Just tell us what you’re making, the dimensions, what it’s going to do, and we’ll send over a quote fast. No BS, just honest, high-quality copper turning.
Aluminum Turned Parts References
ASM International. (2016). Machining of Copper Alloys. ASM Handbook Volume 16: Machining.
DeGarmo, E. P., Black, J. T., & Kohser, R. A. (2020). Materials and Processes in Manufacturing (13th ed.). Wiley.
Machining Cloud. (2023). Dimensional Tolerances in Turning: Best Practices for Soft Metals. Machining Industry Report.
Huizhou Quanyi Precision Hardware Products Co., Ltd.
We’re well-known as one of the leading copper turning manufacturers and suppliers in China, featured by quality products and good service. Please rest assured to buy customized copper turning made in China here from our factory. Contact us for more details.
Address: Building A10, 7th Floor, Zhongchuangyingke 5G Industrial Park, Zhonghan Industrial Park, Tonghu Town, Huizhou City
E-mail: info@qycncturning.com
WebSite: https://www.qycncturning.com/
